

News center
Which ASTM A924 Thickness Tolerances Apply to Galvanized Steel Sheet Coil?
Quality teams inspecting galvanized steel sheet coil must select the correct ASTM A924 tolerance table before accepting material.
The applicable limit depends on the specified product standard, ordered thickness, sheet width, measurement location, and ASTM edition.
For most galvanized sheet, ASTM A653 defines the product requirements, while ASTM A924 supplies general requirements, including dimensional tolerances.
Using an unsuitable tolerance can cause false rejection, unnoticed under-thickness material, fabrication difficulties, and avoidable compliance exposure.
This guide explains how quality and safety personnel can establish practical acceptance criteria for each galvanized steel sheet coil shipment.
What Is the Core Inspection Decision?
The first decision is whether the purchase order identifies ASTM A653, another applicable product specification, or a customer-specific requirement.
ASTM A924 should then be read together with that product specification and the edition referenced by the contract documents.
Do not choose a thickness limit from a generic internet chart without confirming the applicable table, units, and ordering basis.
A galvanized coil may be supplied with different widths, thicknesses, coating designations, and mechanical requirements within one production program.
Each combination may require a separate inspection record and a separate comparison against the relevant tolerance requirement.
The correct acceptance question is therefore simple: does the measured product satisfy the specified standard and ordered dimensions under recognized conditions?
How ASTM A924 and ASTM A653 Work Together
ASTM A924 establishes general requirements for metallic-coated steel sheet, including dimensions, testing, workmanship, and certain delivery conditions.
ASTM A653 covers hot-dip galvanized and galvannealed sheet, including coating designations, mechanical properties, chemical requirements, and ordering information.
When galvanized sheet is purchased to ASTM A653, A924 dimensional provisions commonly support the inspection process.
However, the purchase order remains critical because contractual requirements can modify, supplement, or clarify standard requirements.
Quality personnel should record the exact specification designation, year or edition, grade, coating designation, thickness, width, and delivery condition.
If the order references only “galvanized steel coil,” the supplier should clarify the governing standard before production or final acceptance.
This step prevents later disagreements caused by different interpretations of nominal dimensions and tolerance measurements.
Does Thickness Include the Zinc Coating?
For routine dimensional inspection, galvanized sheet thickness is generally evaluated as the delivered sheet thickness, including the metallic coating.
The coating contributes to the measured overall thickness, although its contribution is usually small compared with the steel substrate.
A mill certificate may separately report nominal steel thickness, coating designation, and measured dimensional results, so records must be read carefully.
Confusing base-metal thickness with total delivered thickness can create an incorrect comparison against the A924 thickness tolerance.
Where a customer specifies base-metal thickness, effective steel thickness, or a special calculation, that requirement must be documented separately.
Do not assume that a micrometer reading automatically represents substrate thickness after coating has been applied.
For disputes, the parties should agree on the measurement method, instrument resolution, sampling locations, and governing standard before testing.
A clear inspection plan should identify whether the reported value is total sheet thickness, estimated substrate thickness, or another contractual measurement.
Which Factors Select the Correct Tolerance?
ASTM A924 thickness tolerances are selected using the ordered thickness and the applicable sheet width range shown in the current standard.
The ordered thickness normally identifies the relevant row, while width determines the applicable column or tolerance category.
Because table layouts and requirements may change between editions, inspectors should use the edition named in the purchase documents.
When no edition is stated, the buyer and supplier should agree on the governing edition before resolving a dimensional claim.
Nominal thickness alone is insufficient when the coil contains multiple slit widths or when the order uses special dimensional terminology.
Inspection personnel should verify whether the width refers to the original coil width, slit width, or finished sheet width.
Slitting can produce edge conditions that affect measurement handling, even though the material originated from a wider master coil.
For safety-related applications, the quality plan should identify the narrowest finished width and the most restrictive applicable tolerance.
This approach reduces the risk of accepting material that meets a broad coil description but fails the actual fabricated dimensions.
How Should Thickness Be Measured?
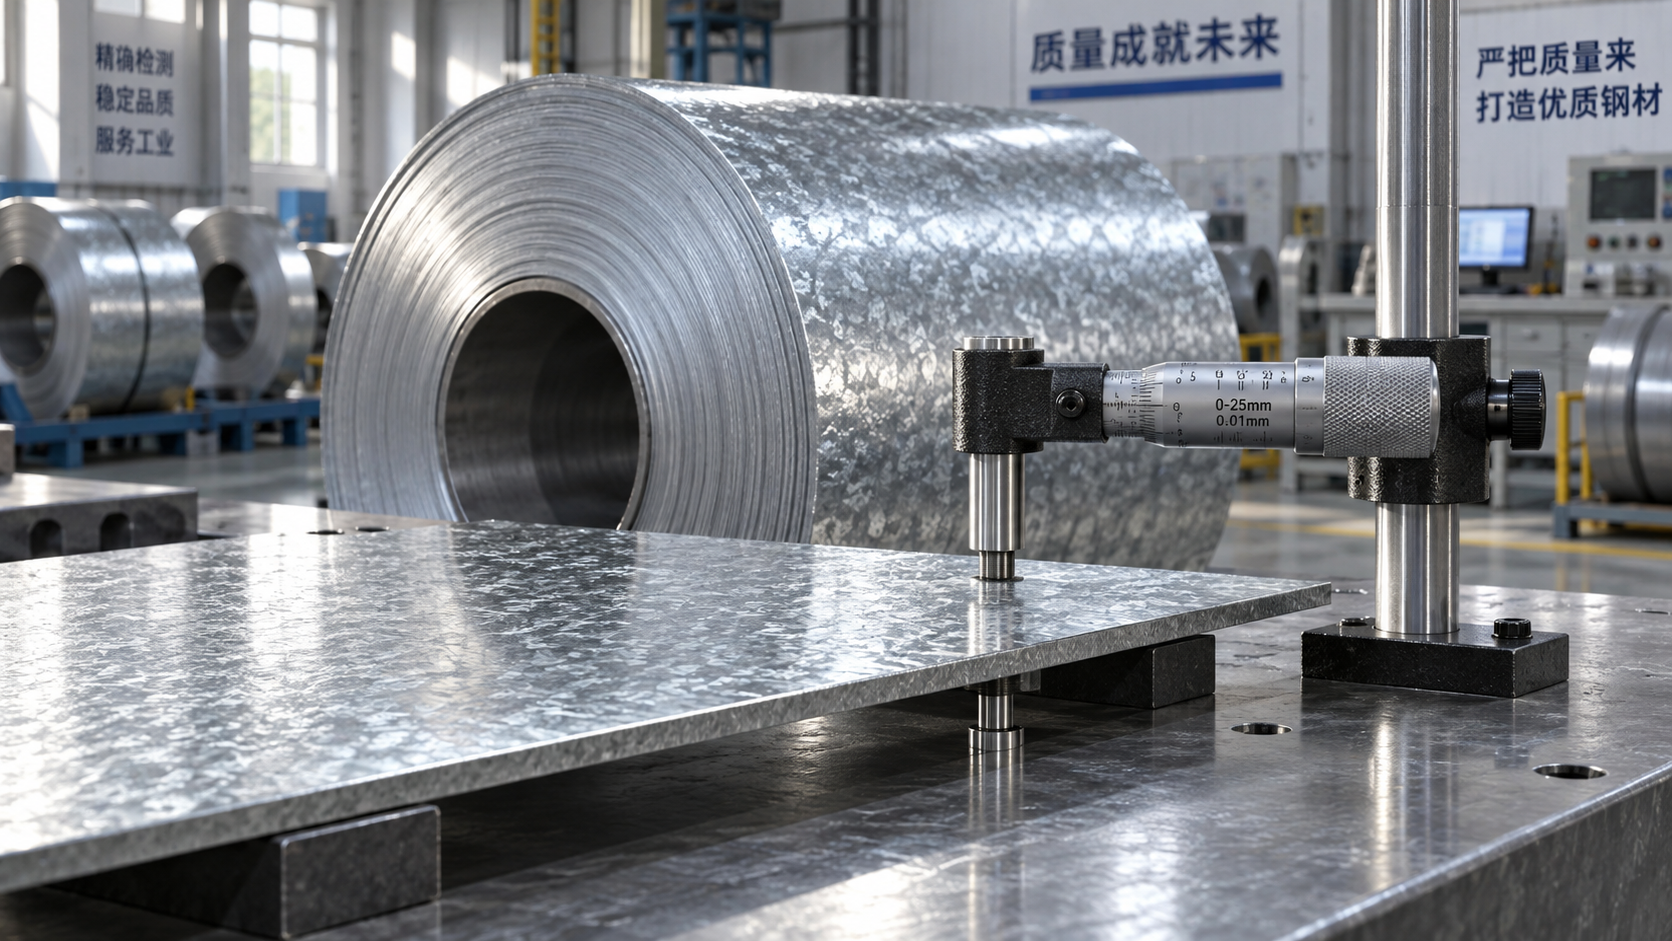
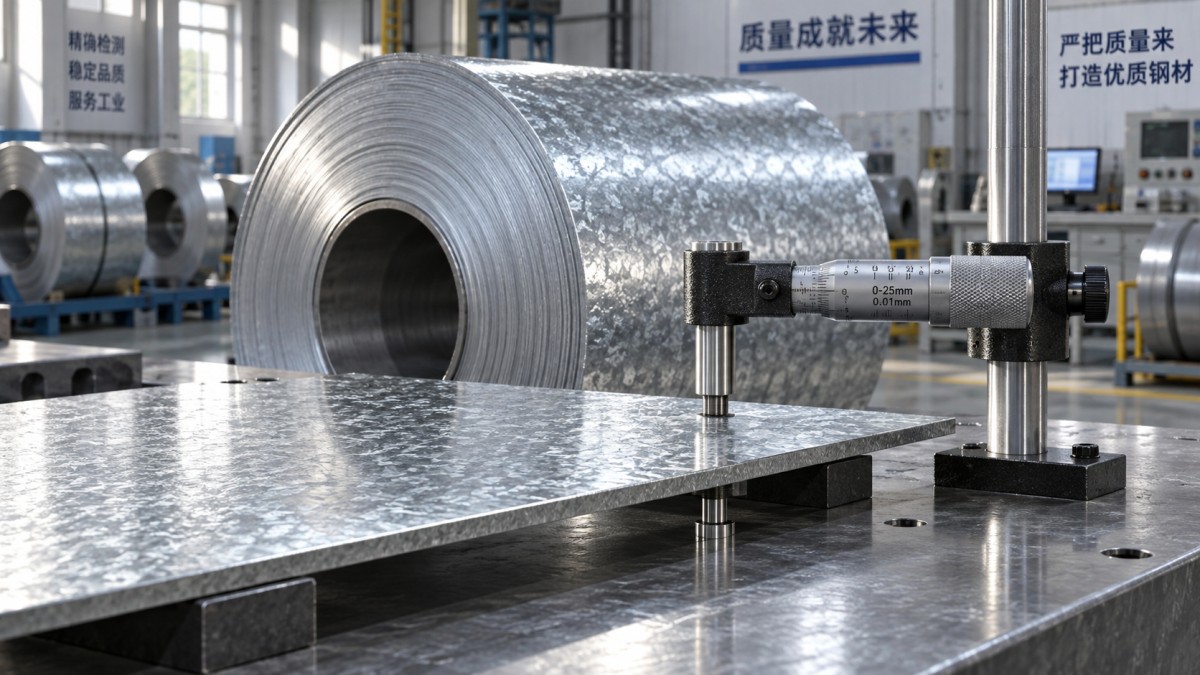
Use a calibrated micrometer or suitable thickness gauge with a measurement range and resolution appropriate for the ordered thickness.
Confirm calibration status before inspection, and record the instrument identification in the quality report.
Measurements should be taken at locations permitted by the applicable ASTM requirement, away from edges where edge effects may distort results.
Do not measure directly over heavy zinc buildup, damaged edges, burrs, dents, or visibly abnormal surface areas.
At the same time, abnormal areas should not be ignored if they indicate a broader manufacturing or handling problem.
Inspectors should separate dimensional acceptance from workmanship evaluation, then document both findings in the same release record.
Before measuring a coil, allow the instrument and material to reach stable workshop conditions when temperature differences could influence readings.
Keep the contact faces clean and apply consistent pressure without compressing the sheet or damaging the coating.
Take multiple readings across the width and along the coil length according to the approved inspection plan.
Random isolated readings may not reveal systematic variation caused by rolling, coating, tension-leveling, or slitting conditions.
When results approach the tolerance boundary, increase the sample size and review the measurement method before making a final decision.
How Can Quality Teams Avoid False Rejection?
A result slightly outside an expected value may reflect an incorrect table, unsuitable instrument, or inconsistent measurement location.
Before rejecting material, compare the purchase order, mill certificate, standard edition, and inspection report line by line.
Check whether the reported thickness is nominal, minimum, average, or an individual measured value.
Confirm that the measured width and thickness match the dimensions used to select the tolerance table.
Review whether the product was supplied as coil, cut sheet, slit coil, or a processed component.
Processing operations can introduce burrs, local deformation, or edge conditions that should be evaluated separately from mill dimensional conformity.
If the customer has approved a special tolerance, that approval should appear in the order, technical agreement, or inspection plan.
Verbal instructions are difficult to defend during an audit and can create inconsistent decisions between shifts or facilities.
For borderline results, preserve representative samples, photographs, instrument records, and the original coil identification.
This evidence supports a technical review and helps distinguish a true nonconformity from a documentation or measurement error.
What Should the Inspection Report Contain?
A useful report identifies the supplier, heat number, coil number, specification, grade, coating designation, ordered thickness, and width.
It should also state the standard edition, measurement instrument, calibration reference, sampling plan, and individual readings.
Record the measurement position, such as operator side, center, drive side, head, middle, or tail location.
Use consistent units throughout the report, and clearly identify any conversion from inch-based values to metric values.
Do not round a borderline result before comparing it with the specified tolerance unless the governing procedure allows that practice.
Keep the unrounded reading available so another reviewer can reproduce the acceptance decision.
The report should state the acceptance basis instead of merely writing “passed” or “failed.”
For example, it can identify the applicable A924 table, ordered dimension, measured range, and resulting conformity decision.
When testing is performed by an outside laboratory, confirm that its procedure matches the contractual dimensional requirements.
Clear reporting improves supplier communication and helps production teams decide whether material can proceed to forming, welding, or coating.
Why Thickness Tolerance Matters for Safety and Fabrication
Thickness variation affects mass, section capacity, forming behavior, weld preparation, and the fit of assembled components.
In structural or pressure-sensitive applications, under-thickness material can reduce the design margin assumed by engineering calculations.
In fabrication, excessive variation may cause inconsistent bending radii, uneven overlaps, dimensional mismatch, or unstable feeding through equipment.
Coating damage can also increase when operators compensate for unexpected thickness or shape variation during forming.
Safety personnel should therefore treat dimensional control as part of material risk management, rather than as a paperwork exercise.
The consequence of nonconforming coil depends on the application, but the inspection principle remains consistent and traceable.
Material used for construction, machinery, transportation, energy equipment, or hardware processing may require different downstream controls.
Purchasing teams should communicate the final application to suppliers when ordinary standard requirements do not fully describe the risk.
That information can support appropriate grade selection, coating selection, processing allowances, and inspection frequency.
Reliable acceptance criteria reduce production interruptions while protecting users from avoidable material-performance uncertainty.
How Should Suppliers and Buyers Resolve Unclear Requirements?
Start with a written technical clarification listing every dimension and standard referenced by the purchase order.
Ask the supplier to identify the exact A924 table, product specification, edition, and measurement basis used during production inspection.
Compare that information with the buyer’s intended finished product and fabrication process.
If the coil will be slit, leveled, cut, punched, or bent, define which stage controls dimensional acceptance.
Clarify whether the supplier’s certificate reports mill readings, final processed readings, or both.
Where special tolerances are needed, place them directly in the order and obtain written supplier acknowledgment.
For repeated purchasing, create a controlled material specification that defines standard edition, tolerances, sampling, documentation, and nonconformity handling.
This reduces interpretation differences across suppliers, purchase orders, warehouses, and production locations.
A dependable metal supplier should be able to explain its inspection process and provide consistent traceability for each coil.
For customers requiring related corrosion-resistant products, the Galvalume Steel Coil may also be evaluated separately according to its applicable product standard and coating requirements.
Practical Receiving Checklist for Galvanized Coil
Before unloading, verify coil identification, packaging condition, labels, quantity, and visible transport damage.
Match the label with the purchase order, certificate, heat number, coating designation, thickness, and width.
Check whether moisture staining, edge damage, telescoping, or handling marks require additional evaluation before acceptance.
Measure thickness using calibrated equipment at planned locations, maintaining consistent contact pressure and measurement technique.
Compare every result with the correct A924 requirement for the ordered dimension and applicable width category.
Record readings before rounding, and preserve the original inspection data with the receiving documentation.
Inspect width, flatness, shape, surface condition, and coating appearance where those characteristics affect fabrication or service safety.
Quarantine questionable coils until the quality team completes technical review and communicates a documented disposition.
Release material only when identity, dimensions, coating requirements, and supporting documents satisfy the approved acceptance plan.
This process creates a repeatable control point between supplier shipment, warehouse storage, and manufacturing use.
Final Guidance for Applying ASTM A924 Tolerances
The correct ASTM A924 thickness tolerance cannot be selected from thickness alone.
Quality personnel must connect the product specification, standard edition, ordered thickness, applicable width, measurement method, and contractual requirements.
For galvanized steel sheet coil, ASTM A653 commonly provides the product framework, while A924 supports general dimensional and delivery requirements.
Always determine whether the inspection concerns delivered total sheet thickness or a specifically ordered base-metal thickness.
Use calibrated equipment, approved measurement locations, documented sampling, and unrounded readings for borderline decisions.
When requirements are unclear, obtain written clarification before production or acceptance, especially for safety-critical applications.
A disciplined inspection method protects purchasing decisions, improves fabrication reliability, and gives safety teams evidence they can defend.
By controlling the tolerance selection process, companies can accept conforming material confidently and address genuine nonconformities quickly.
Please give us a message