

News center
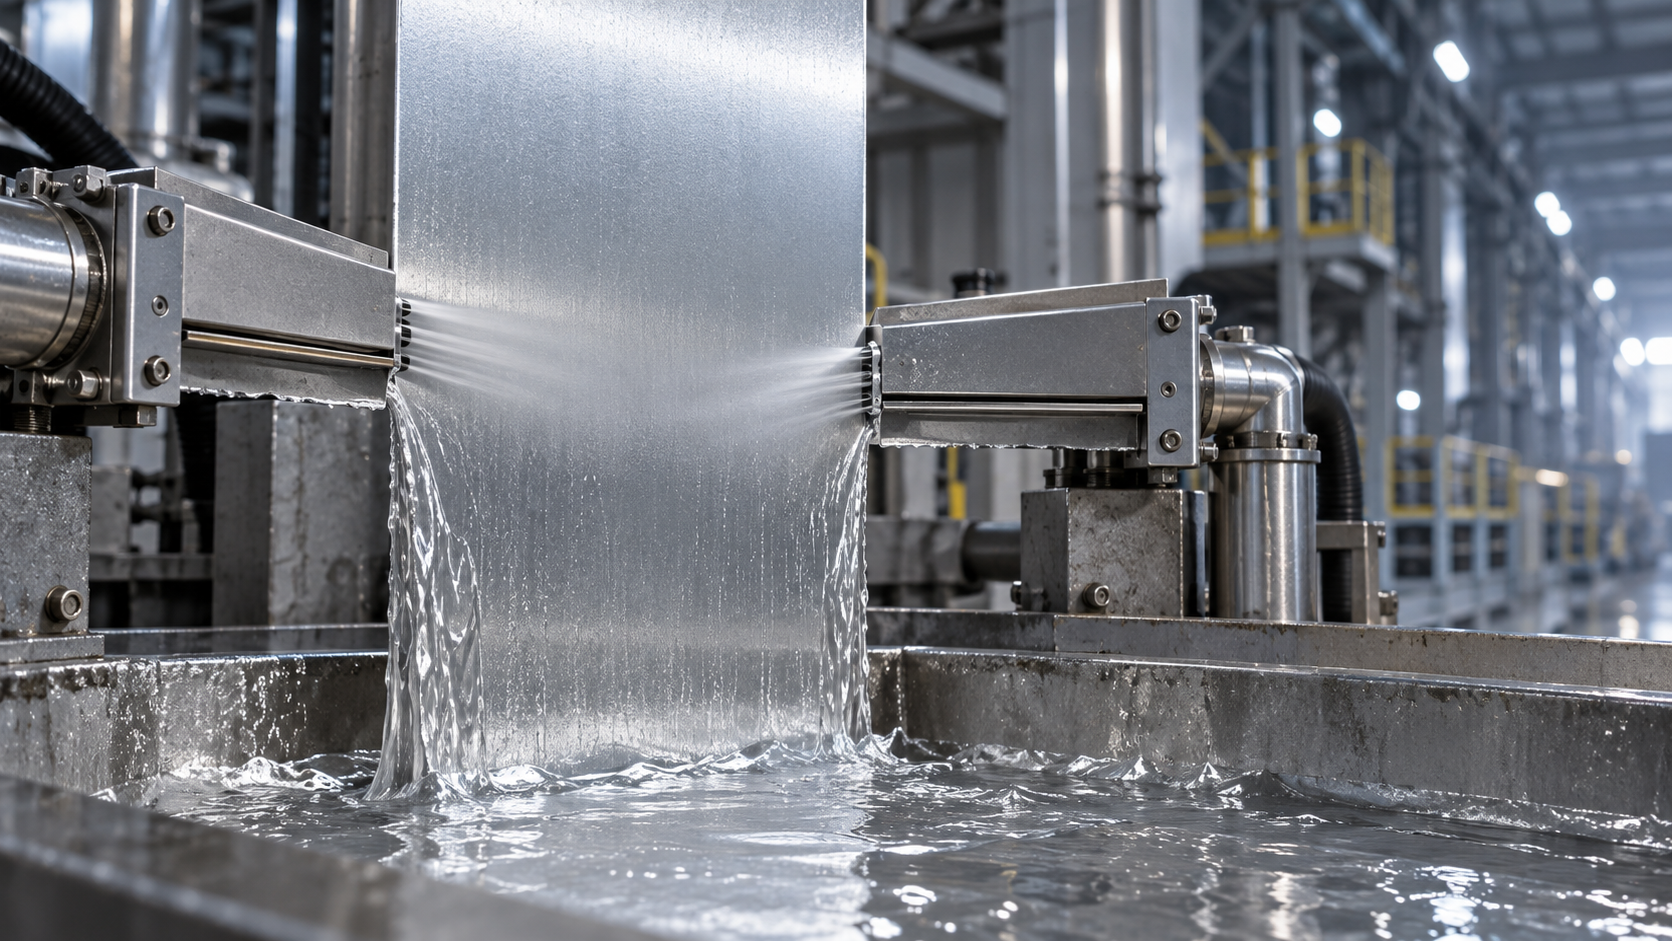
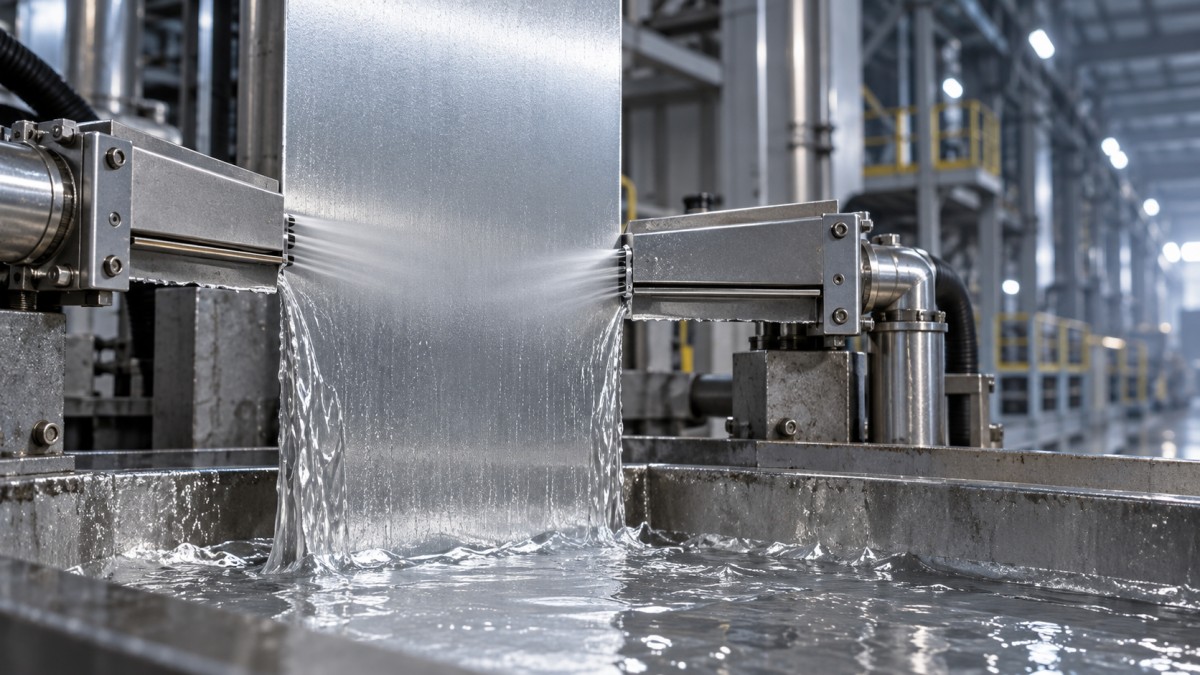
Air knives control coating uniformity on hot dipped galvanised coil by metering the liquid zinc film before it solidifies. Their performance depends on the pressure and shear delivered at the strip surface—not simply the gas pressure displayed at the supply manifold. A stable average coating mass can therefore coexist with heavy edges, a thin centre band or unequal coatings on the two faces.
The central control problem is to remove enough zinc to reach the specified coating mass while maintaining an acceptable distribution across the width, along the length and between faces. Gas pressure, nozzle geometry, stand-off distance and strip speed must be treated as a coupled system. Increasing pressure alone cannot correct a distorted strip, damaged nozzle lip or unstable pass line.
How the gas jet meters the liquid zinc film
As steel strip rises from the zinc bath, it carries a liquid film whose initial thickness depends on withdrawal speed, bath properties and the condition of the strip surface. Opposed slot nozzles direct gas jets towards the two faces. Near each jet’s impact region, the resulting pressure gradient and gas shear drive excess liquid zinc downwards, opposing the upward transport caused by the moving strip.
The film that passes above this wiping region becomes the final metallic coating after cooling and solidification. Air knives therefore regulate the removable liquid portion of the coating; they do not independently determine the steel–zinc interfacial reaction. Bath chemistry, strip temperature and immersion conditions remain important, particularly where intermetallic growth contributes appreciably to the coating structure.
The term “air knife” also describes systems using nitrogen rather than compressed air. Gas selection changes oxidation behaviour and operating cost, but the basic metering mechanism remains a gas jet acting on a moving liquid film. Neither gas choice guarantees a uniform result without stable nozzle and strip geometry.
Three different uniformity questions need separate answers:
- Cross-width uniformity: whether the coating profile remains within the required limits from one side of the saleable strip to the other.
- Longitudinal uniformity: whether coating mass stays controlled during steady running, speed changes and other process disturbances.
- Face-to-face balance: whether each surface receives its intended coating, rather than merely achieving the correct combined total.
A single coil-average value cannot establish all three. The distinction matters when one face will undergo severe forming, remain exposed to corrosion or receive a subsequent surface treatment.
Pressure only works through nozzle geometry and stand-off
For a fixed nozzle arrangement and stable operating conditions, increasing gas pressure generally strengthens wiping and reduces the retained zinc film. The relationship is not a universal linear calibration. Compressible gas flow, nozzle losses, jet development and liquid-film behaviour prevent a pressure setting from being transferred directly between different lines or knife designs.
The nozzle slot establishes the initial jet thickness and influences gas flow. Its opening must be consistent across the working width. Lip damage, deposits, thermal distortion or incorrect adjustment can create local differences in jet momentum, leaving longitudinal coating bands even when the pressure supply appears stable. Changing overall pressure may shift the average coating mass while leaving these bands largely intact.
Stand-off—the distance between the nozzle exit and the strip—determines how the jet develops before impact. Increasing this distance allows the jet to spread and changes its peak pressure and pressure footprint. Reducing the distance can improve wiping effectiveness, but leaves less clearance for strip movement, shape defects and weld passage. The useful setting is therefore constrained by mechanical stability, not just coating-mass response.
The ratio of stand-off distance to slot opening is particularly important when comparing nozzle configurations. Two systems operating at the same supply pressure and absolute stand-off need not produce the same surface pressure distribution if their slot openings differ.
Knife angle and elevation also affect wiping and the return flow of removed zinc. These settings should be assessed against the nozzle design and operating envelope rather than adjusted according to a universal “best angle”. Excessive wiping intensity can promote splashing and unstable liquid flow, creating a practical limit to pressure-based correction.
The strip is part of the wiping system
A uniform jet cannot produce a uniform coating if the strip-to-nozzle distance varies significantly across the width or with time. Crossbow changes local stand-off from centre to edge. Lateral movement changes how the strip edges interact with the ends of the jets. Flutter creates a time-varying gap, potentially producing alternating coating variation on opposite faces.
Opposed knife pressures also interact with strip position. An unbalanced pair of jets can exert a net force on the strip, altering the gap that the control system is trying to regulate. Separate pressure adjustment remains necessary for face-to-face control, but its mechanical effects must be considered alongside tension, strip shape and stabilisation.
Increasing strip tension may reduce some movement, but it is not an unrestricted remedy: permissible tension depends on strip dimensions, temperature, grade and line configuration. Electromagnetic stabilisation, where installed, can reduce motion near the wiping zone. It does not replace correct knife alignment, nozzle maintenance or appropriate pass-line control.
Evidence of stable pressure is consequently insufficient evidence of stable wiping. A meaningful process assessment connects pressure records with strip position, vibration, width, thickness and speed under the same production conditions.
Why speed changes expose control weaknesses
At unchanged wiping settings, increasing withdrawal speed generally increases the liquid zinc carried upwards and tends to increase the retained coating. A suitable control system anticipates this response rather than waiting for a downstream gauge to detect excess coating.
Feedforward control applies settings derived from line speed, target coating mass and relevant product variables. Feedback then corrects the remaining difference between measured and target coating. The two functions are complementary: feedforward handles predictable changes, while feedback compensates for model error and slower process drift.
The downstream gauge introduces transport delay. If the measurement position is a distance L from the knives and strip speed is v, the travel-time component is approximately L/v. Measurement processing and actuator response add further delay. During acceleration or deceleration, the control system must associate a reading with the strip section and knife settings that produced it, not simply with current operating conditions.
Aggressive feedback without suitable delay compensation can cause repeated overcorrection. Excessively conservative feedback leaves a longer strip length outside the intended operating band after a disturbance. Control performance should therefore be examined during transitions as well as steady running.
Reading coating patterns as evidence
The spatial pattern of a coating deviation helps distinguish an average-setting problem from a geometry or stability problem. These patterns guide investigation; they are not unique diagnoses.
Edge buildup deserves particular attention because the flow near a free strip edge differs from that over the central surface. Jet interaction, liquid redistribution and local strip shape can all contribute. Edge baffles or other edge-control devices may improve the profile, but their position must remain appropriate as strip width and lateral position change.
Raising pressure across the entire width to reduce heavy edges can over-wipe the centre. It may also increase gas consumption and splashing without resolving the underlying edge-flow condition. Centre and edge measurements should therefore remain distinguishable rather than being hidden within a single transverse average.
Not every visible surface defect originates at the knives. Dross particles, poor wetting and subsequent contact damage require different corrective actions. A streak or rough patch should be correlated with coating mass, surface appearance and process history before it is classified as a wiping defect.
Connecting process measurements to coating standards
Coating mass and coating thickness are related but are not interchangeable reporting terms. Coating mass is commonly expressed in grams per square metre, while thickness is expressed in micrometres. The conversion requires the coating density and a clear statement of whether the mass covers one face or both.
For illustration, a combined coating mass of 275 g/m², equally divided between the faces and treated as pure zinc with a density of approximately 7.14 g/cm³, corresponds to about 19.3 μm per face. This is a nominal conversion, not proof that either face meets a local thickness requirement. Unequal coating distribution and alloy-layer composition can affect the interpretation.
EN 10346 and ASTM A653/A653M are relevant product standards for continuously hot-dip-coated steel sheet, with different designation and acceptance frameworks. ASTM A90/A90M provides coating-mass test methods within its scope. The applicable edition, coating type, sampling provisions and purchase specification must be identified before judging compliance. ISO 1461, which addresses hot dip galvanised coatings on fabricated iron and steel articles, is not the appropriate substitute for a continuously galvanised sheet specification.
Online gauges provide valuable process coverage, but their readings must be supported by calibration and suitable reference testing. Measurement can be affected by coating composition, substrate characteristics, geometry and the gauge’s measurement principle. It is also necessary to establish whether the reported signal represents one face, a combined result or a calculated value.
A traversing gauge does not capture every cross-width point at the same instant. During rapid process changes, part of an apparent transverse profile can reflect longitudinal variation occurring while the gauge scans. Profile interpretation must therefore account for scan timing and strip travel.
What demonstrates effective air-knife control
A credible assessment starts with a defined coating target and acceptance basis, then examines performance over the relevant width, gauge and speed range. Useful evidence includes individual-face coating profiles where available, longitudinal variation, transition lengths, nozzle condition and synchronised operating records. Samples used for reference testing should be traceable to the corresponding process data.
The most revealing comparison is not simply whether two coils have the same average coating mass. It is whether their local low points, edge buildup, face balance and transition behaviour are controlled to the required limits. Excess zinc added as a safety margin may hide process variation, but it does not demonstrate tighter control.
Air knives perform effectively when the gas-flow system, strip geometry and measurement loop remain stable together. The practical objective is a reproducible coating distribution with sufficient margin to meet the specified acceptance criteria—not the lowest pressure, the highest jet intensity or the most favourable coil average.
Please give us a message